Stepped shafts
Specify the locating diameters, shoulders and datum axis. Show any cross-holes or flats and identify the surfaces that contact another component.
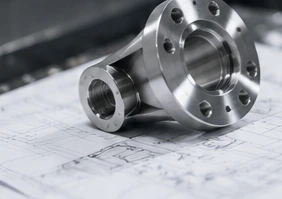
Specify the locating diameters, shoulders and datum axis. Show any cross-holes or flats and identify the surfaces that contact another component.
Define the bore, outside diameter and end-face requirements together. Include the mating material and any friction, cleaning or surface-treatment restrictions.
Identify the locating diameter, bolt pattern and sealing face. For fluid-contact parts, include the operating environment and any required acceptance tests.
Mark the faces and holes that locate the bracket in the assembly. Share load-critical features, edge requirements and any areas where a design change is permitted.
Show the hole pattern, flatness and parallelism requirements. Identify the inspection support condition and surfaces that must remain free from handling marks.
Include intersecting bores, thread details and internal edge requirements. Discuss access for machining, cleaning and inspection before releasing the drawing.
Grade 2 is commercially pure titanium, used in industrial equipment where corrosion resistance and formability matter. It is a different material specification from Ti-6Al-4V. [1]
Grade 5 is the Ti-6Al-4V alloy. It is widely used for mechanical components where strength and weight are important; its properties depend on the material condition and processing history. [2]
Grade 23 is the extra-low-interstitial variant of Ti-6Al-4V, with tighter limits on certain elements. It should be specified and documented as ELI, not treated as an automatic substitute for Grade 5. [2]
Specify the titanium grade, governing standard and edition. Material availability is confirmed during quotation; any alternative requires your approval.
| Property | Ti-6Al-4V, annealed TIMETAL 6-4 bar | Condition |
|---|---|---|
| Minimum tensile strength (MPa) | 895 | Annealed; section <76.2 mm |
| Minimum yield strength (MPa) | 828 | 0.2% offset; 20°C |
| Minimum elongation (%) | 10 | Longitudinal specimen |
TIMET TIMETAL 6-4, Table 3: published minimum values for annealed ASTM B348 bar or sections below 3.00 in (76.2 mm), tested longitudinally at 20°C.
Share the CAD model with the dimensioned drawing. The review covers pocket access, internal corners, wall support and the order in which faces and holes are finished. Multi-face work may need more than one setup.
View the Machining ServiceIdentify the datum axis, shoulder positions, thread requirements and mating components. Long or thin sections need a workholding and inspection plan that reflects the finished part, not only how the stock is held.
View the Machining ServiceFor inclined holes and contoured faces, compare practical setup options before specifying a machine type. The proposed route should explain how the required features are reached and checked.
View the Machining ServiceTitanium alloys conduct heat poorly compared with many common machining metals, so heat and tool wear need attention at the cutting edge. Tool choice and cutting conditions must be planned for the actual grade and part. [3]
Identify both mating materials, thread class and whether the assembly will be opened repeatedly. List permitted lubricants, coatings or inserts so they can be reviewed with the design owner.
Describe the contact surface, mating component, load and movement. A smooth appearance does not define an acceptable friction or wear condition; state the required treatment and acceptance criteria.
Mark the sealing land, surface-finish requirement and internal edges. Specify the service medium and any cleaning, leak-test or residue requirements that must be included in the quoted scope.
Separate cosmetic surfaces from functional contact surfaces. Provide a finish specification or approved reference sample and identify any areas that must not be blasted, colored or marked.
No assembly requirement selected.
Show the smallest wall sections and the faces that may be held during machining. Identify whether flatness or position is measured freely supported or under a specified assembly condition.
A drawing review should resolve tool access, internal radii and features hidden behind other surfaces. Mark which radii can change and which are functionally fixed; do not leave those decisions to an unrecorded assumption.
State full thread depth separately from drilled depth. Identify cross-hole intersections and edges where a burr is unacceptable. Specify the checking method where a feature is difficult to inspect directly.
Include stock-direction requirements where the design calls for them. Any stress relief, heat treatment, joining or specialist finishing should be part of an agreed route, with final acceptance after the relevant operations.
No review topics selected.
| Feature | Specification | Acceptance condition | Verification |
|---|---|---|---|
| Diameters and mating fits | Size limits; fit; datums; final surface condition | Specified measurement stage; later-process allowance | Final size and fit checks |
| Flatness, position and runout | Datums and controlled features | Free-state or defined support | Reported assembly-critical geometry |
| Threads and internal features | Thread standard/class; full depth; intersections; edges | Specified stage relative to finishing | Gauges or specified verification method |
| Surface texture and treated areas | Roughness parameter/units; locations; masking; process specification | Specified treated and masked areas | Separate roughness, appearance and treatment records |
Achievable limits depend on size, geometry, grade, condition and processing, so we confirm the tolerance for your titanium part rather than quoting one figure for all of them. Mark the critical features on the drawing and have them confirmed in the quotation.
Specify allowable tool marks, edge breaks and cleanliness. Identify any surfaces that require a measured roughness or additional finishing, rather than relying on “smooth” as the complete instruction.
Define critical edges and packing protection.
For a specified blasted appearance, agree the media, surface zones, masking and reference sample. Keep threads, fitted bores and sealing areas explicitly included or excluded from the process.
Agree appearance separately from dimensions.
Titanium color anodizing and a functional anti-galling treatment are not the same requirement. Tiodize distinguishes its color-producing Type III process from its anti-galling Type II process. [4]
State the actual specification; color alone is not proof of wear performance.
For friction, wear or another functional requirement, send the approved process specification and acceptance criteria. We will review the specialist route, masking, inspection and production responsibility before quoting.
Specialist treatment is subject to scope and supplier review.
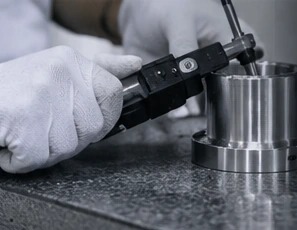
Specify the required material documentation and whether it must be reviewed before the stock is cut. Link the grade, product form and condition to the actual supplied material, not to a general datasheet.
Specify the required heat, batch or individual-part traceability. Agree how material identity is retained through machining, finishing and packing.
Identify reportable dimensions, sampling and measurement setup. A dimensional report, material certificate and finishing record answer different questions and should be specified separately.
Define separation of parts, protection of edges and any restrictions on residues or marking. Agree how to document a discrepancy on arrival and which batch information should accompany it.
Identify whether the sample is for fit, assembly or functional testing. Where material properties matter to the test, agree the representative grade and condition instead of changing them simply to obtain a faster sample.
Record drawing changes, finish acceptance and inspection results before releasing a batch. The release also confirms the agreed price, delivery terms and required records. Keep accepted deviations separate from the next controlled drawing.
Include the part number, revision, quantity and required records on every release. Tell us when the mating component, application or specification changes, even if the part geometry appears unchanged.
A quotation should distinguish the material requirement from the machining work. Stock dimensions, certification, excess material and any approved alternative affect how the job is planned.
Deep pockets, small features, multiple setups and extra finishing can change the scope. Request separate options where a permitted design adjustment could simplify machining, without changing a functional requirement.
List sample quantities, production quantities, reports and release dates together. Compare quotations for the same grade, finish, inspection scope and delivery responsibility rather than comparing a unit price alone.
Use the grade on your approved drawing, together with the material standard and supplied condition. Grade 2 is commercially pure titanium; Grade 5 and Grade 23 belong to the Ti-6Al-4V family. They are not interchangeable specifications. [1] [2]
Grade 23 is the extra-low-interstitial variant of Ti-6Al-4V, with tighter limits on certain elements. State ELI and the applicable product standard when required. Ask for the relevant material documentation rather than relying only on a trade name. [2]
Yes. Send the full designation, required edition, stock form, condition and documentation requirements. Feasibility and supply must be reviewed for the actual order. A similarly named grade should not be substituted without your approval.
Titanium alloys place particular demands on cutting tools because heat is concentrated near the cutting edge and tool wear can be challenging. The grade, feature geometry and required finish should be reviewed together when planning the machining route. [3]
Provide the critical limits, datums, surface condition and measurement requirements. Achievable tolerances depend on diameter, wall thickness and processing route and must be confirmed for your drawing in the quotation.
Do not use color as evidence of anti-galling performance. Tiodize distinguishes its color-producing Type III process from its functional Type II treatment. Specify the required process and performance; do not substitute a decorative finish for a functional one. [4]
Send the qualification, approved-source, traceability and documentation requirements before ordering. Application approval rests on the qualification, approved-source, traceability and documentation requirements you send before ordering. We will review the required scope rather than imply that every titanium component is suitable for a regulated use.
Show the mating material, thread or fit specification, surface finish and assembly conditions. Identify permitted lubricants, coatings or inserts and any restrictions on residues. The design owner should approve the contact-surface arrangement.
Yes. List the quantities and release stages separately, along with any sample approval or validation requirements. The practical quantity, price and schedule are confirmed after reviewing the drawing, material and process scope.
List material certification, heat or batch traceability, dimensional reports and finishing records in your inquiry. Specify whether documents need approval before machining. The quotation should confirm which records are included and any additional checks required.
We can discuss a suitable partner, coordinate the work or introduce you directly. Responsibilities, commercial terms and communication should be agreed before the order is released.
Agree confidentiality and a suitable file-transfer method before sharing sensitive or restricted information. The inquiry form accepts STEP, IGES, PDF, DWG, DXF, SLDPRT and ZIP files up to 20 MB.
Agree confidentiality and the transfer method before sharing sensitive or restricted files.
Share your drawing, material and quantity. Tell us what you need and we will reply by email.
Material and machining references. Use the current governing specification and order-specific material records alongside the approved drawing.
We use Google Analytics to see how this site is used. Analytics cookies are set only if you accept. Privacy Policy
